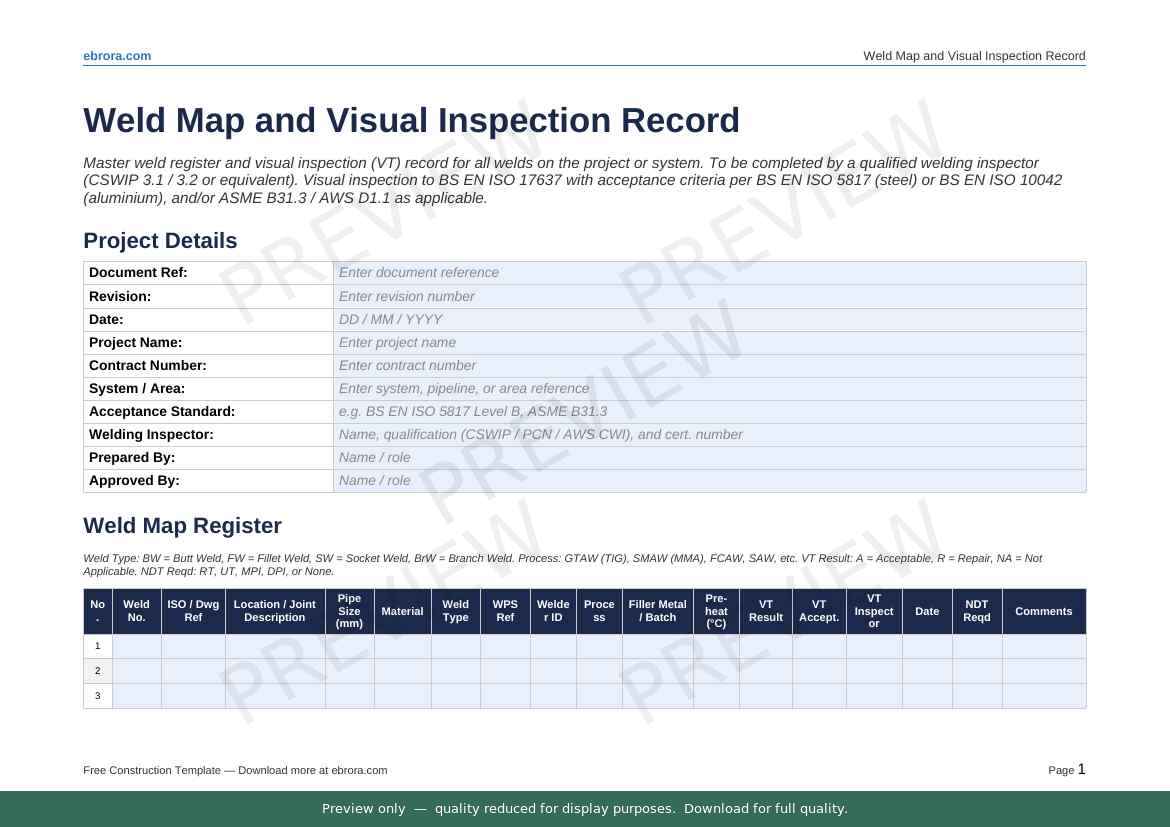
The weld docket is a consolidated collection of critical quality and technical records documenting the entire lifecycle of a specific weldment or project. It serves as an essential evidence package for regulatory compliance, quality assurance (QA), and structural integrity verification, ensuring that every weld adheres to specified engineering codes and safety standards.
The Purpose and Significance of the Weld Docket
In industrial fabrication, aerospace, civil infrastructure, and pressure vessel manufacturing, a weld is rarely just a physical joint; it is a point of potential failure. Consequently, the weld docket serves as the authoritative "birth certificate" for these joints. Without a properly assembled docket, a project may fail mandatory inspections, face costly rework, or be deemed non-compliant with jurisdictional safety laws.
The primary role of the docket is to provide traceability. If a structural failure occurs or if a routine audit is conducted, the docket allows engineers and inspectors to trace the weld back to the specific welder, the exact batch of filler metal used, the calibrated equipment settings, and the results of non-destructive testing (NDT). This transparency is vital for risk mitigation and liability management.
Core Components of a Comprehensive Weld Docket
A professional weld docket is typically structured to follow the flow of the welding project—from initial qualification to final inspection. While requirements vary by sector (e.g., ASME for pressure vessels, AWS for structural steel), most dockets contain the following essential documents:
1. Project Specifications and Design Documents
This section includes the original drawings, engineering specifications, and the specific codes or standards (such as API, ASME, or ISO standards) that govern the project. It establishes the baseline requirements against which all work is measured.
2. Personnel Qualifications
Every individual performing a weld must have documented evidence of their competency. This includes:
- Welder Performance Qualification Records (WPQR): Evidence that the welder has passed standardized tests for the specific process and position they are performing.
- Continuity Logs: Records confirming that the welder has remained active in their trade to maintain certification validity.
3. Welding Procedure Specifications (WPS)
The WPS is a "recipe" for the weld. It specifies the essential variables, such as amperage, voltage, travel speed, shielding gas flow, and preheat/interpass temperatures. A weld docket must contain the specific WPS used for each joint to prove that the process used was validated through a Procedure Qualification Record (PQR).
4. Material Traceability Records
This documents the raw materials used in the construction. It includes Mill Test Reports (MTRs) for the base metal and Certificates of Conformance for filler metals (electrodes, wire, flux). This ensures the chemical composition and mechanical properties match the engineering design.
5. Inspection and Testing Reports
This is the heart of the docket. It contains the results of:
- Visual Inspection (VT): Records from certified inspectors verifying the external quality of the weld.
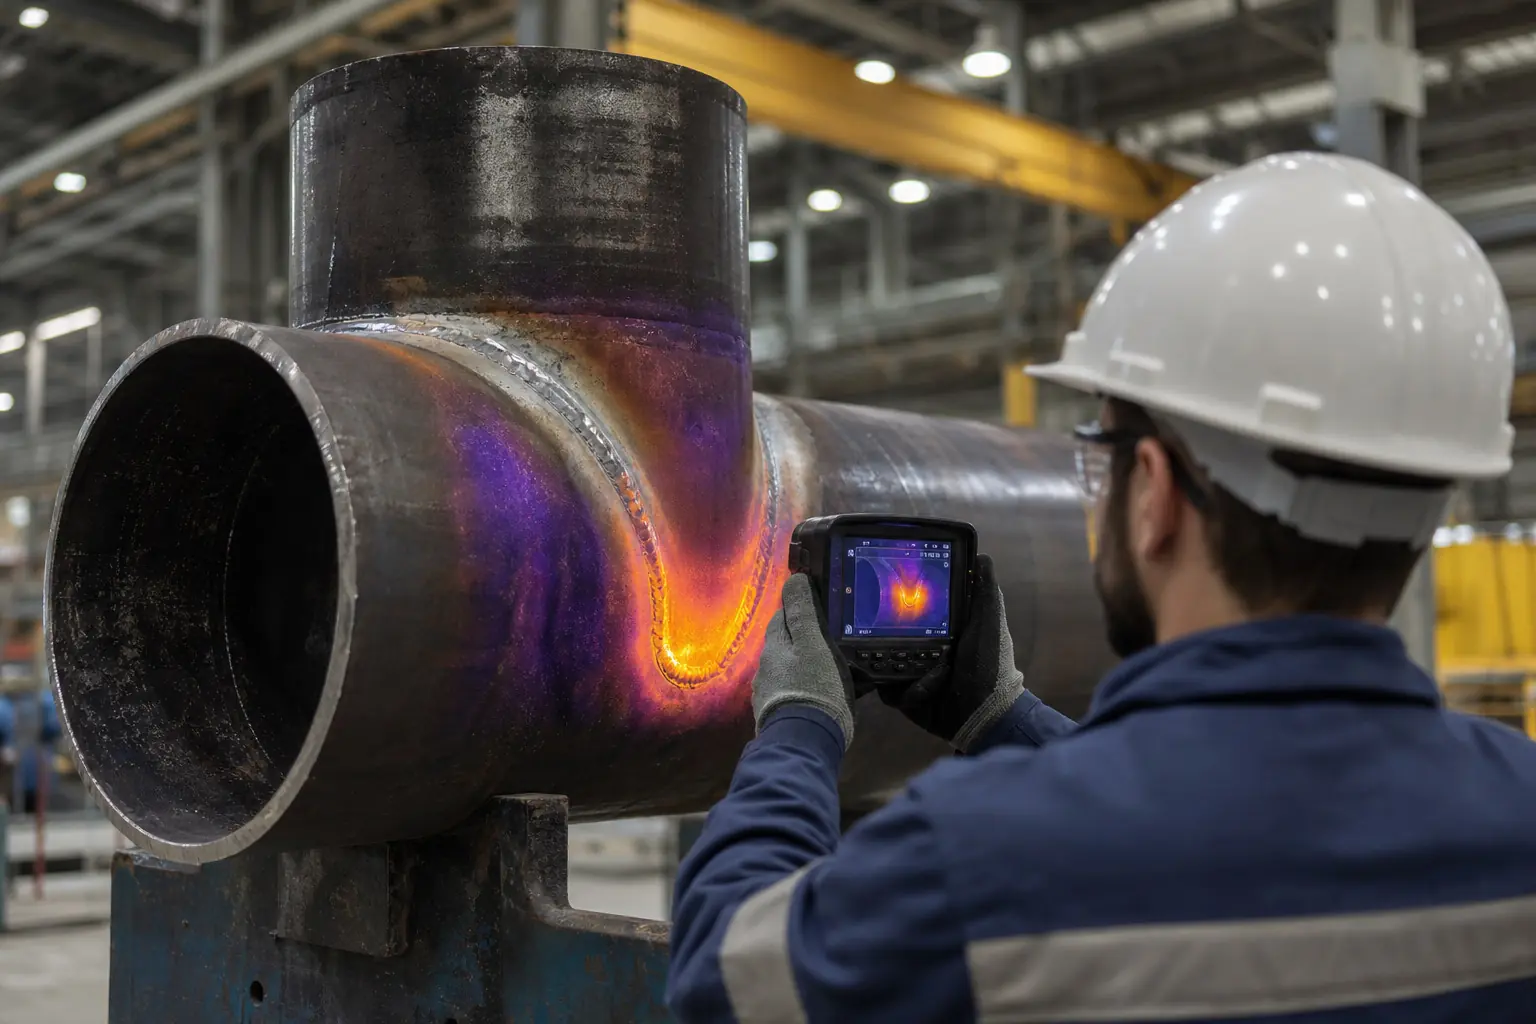
- Non-Destructive Testing (NDT): Reports from ultrasonic (UT), radiographic (RT), magnetic particle (MT), or dye penetrant (PT) testing.
- Pressure Tests: In the case of piping or tanks, hydro-test or pneumatic test certificates.
Practical Management and Traceability
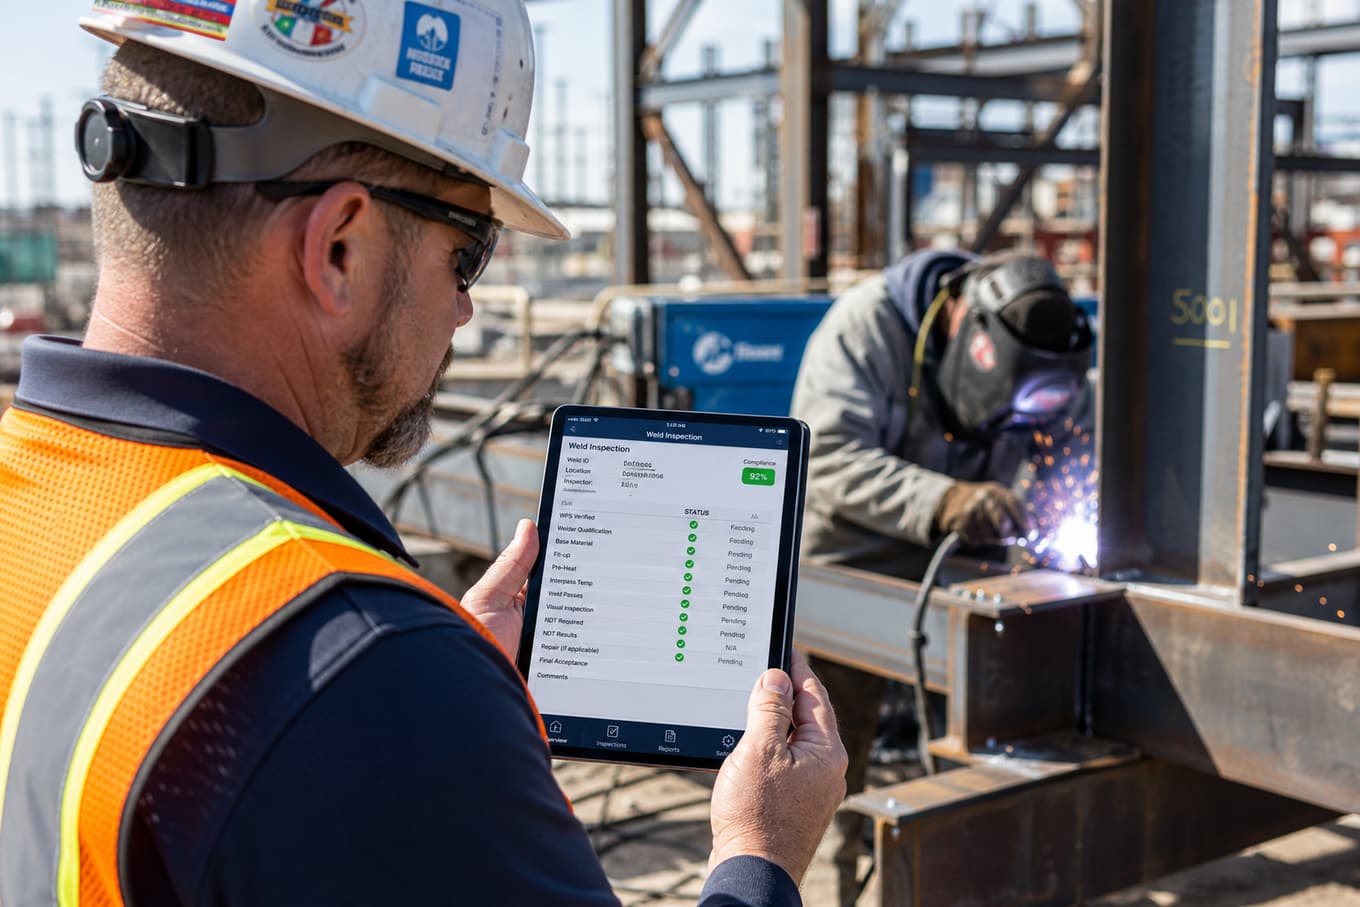
Managing a weld docket requires a rigorous systematic approach. In 2026, many organizations have transitioned from physical paper binders to digital Quality Management Systems (QMS) to prevent the loss of documentation and to ensure immediate accessibility during audits.
Best Practices for Compilation
- Continuous Updates: Do not wait until the end of a project to compile the docket. Create the structure at the project’s inception and add documents as work packages are completed.
- Unique Identification: Assign every weld a unique tracking number (a weld map identifier). This number should appear on the drawings and correspond directly to the entries in the inspection reports.
- Verification Audits: Conduct "mini-audits" throughout the project to ensure that MTRs are correctly linked to the physical materials being installed.
Table 1: Common Documentation Categories and Requirements
| Category | Typical Document Type | Purpose |
|---|---|---|
| Material | Mill Test Reports (MTRs) | Verify chemical and physical properties of steel. |
| Consumables | Batch/Heat Certificates | Confirm filler metal matches WPS requirements. |
| Procedure | WPS and PQR | Prove the welding process is sound and tested. |
| Personnel | Welder Certs (WPQR) | Ensure operators are qualified for the specific task. |
| Inspection | NDT/RT/UT Reports | Validate the finished weld is free of critical defects. |
Legal and Regulatory Compliance
Compliance is the driving force behind the weld docket. Jurisdictional authorities, such as those overseeing boiler safety or structural building codes, mandate that these records be maintained for specific retention periods—sometimes for the entire design life of the asset.
Failing to maintain an accurate docket can lead to:
- Project Stoppages: Inspectors have the legal right to halt operations if traceability is absent.
- Legal Liability: In the event of an accident, the absence of a detailed docket removes a company's primary line of defense in showing that due diligence was performed.
- Insurance Denial: Many industrial insurance policies require proof of certified welding procedures and regular inspections as a condition of coverage.
Troubleshooting Common Documentation Gaps
Discrepancies often occur during high-pressure construction phases. The most common issues include "missing MTRs," where the paperwork for a heat of steel was not collected at the time of delivery, and "expired certifications," where a welder’s qualifications lapsed during the project duration.
To resolve these:
- Retrospective Documentation: If an MTR is missing, contact the supplier immediately to retrieve a duplicate. Never proceed with a weld if the material grade cannot be verified.
- Standardization: Implement a "Hold Point" in the project schedule. No welding can proceed until the supervisor has signed off that the material, personnel, and WPS documentation are verified.
- Digitization: Utilize cloud-based document management that requires mandatory fields to be filled before a record can be saved. This prevents incomplete entries from entering the final docket.
Frequently Asked Questions
What is the difference between a WPS and a PQR in a weld docket?
A WPS (Welding Procedure Specification) is the instruction manual for the welder, while a PQR (Procedure Qualification Record) is the report that proves the WPS actually produces a sound weld when tested. You must have a PQR to support the use of a WPS.
How long must I keep a weld docket?
Retention requirements vary by industry and local law. For pressure vessels, it is often the life of the vessel. For structural steel, it may be 7 to 10 years after completion. Always check your specific project contract and local regulatory guidelines.
Can a weld docket be electronic?
Yes, in 2026, electronic dockets are the industry standard. They must be stored in a secure, backed-up format and remain readable for the duration of the required retention period. Ensure your digital system complies with audit standards for data integrity.
What if I discover a missing inspection report for a completed weld?
This is a critical non-conformance. You must isolate the affected joint, perform a structural assessment, and—if necessary—conduct a new NDT inspection. If the weld cannot be verified, it may require repair or replacement under the supervision of a certified welding inspector.
Who is responsible for the weld docket?
Typically, the Quality Manager or the Lead Welding Engineer is responsible for the integrity of the docket. However, every supervisor and welder has a role in ensuring the data they produce is accurate and submitted to the document control system.
Final Recommendations for Effective Record-Keeping
To maintain a successful weld docket, adopt a "Quality-First" mindset. Do not view the docket as a bureaucratic hurdle, but rather as the final deliverable of your project. If the paperwork is not complete, the project is not complete.
- Start Early: Define your documentation requirements during the pre-construction meeting.
- Appoint a Document Controller: Dedicate a team member to manage the inflow of paperwork daily.
- Audit Regularly: Schedule internal audits of your docket every two weeks during long-term projects to catch gaps early.
- Final Review: Before handover, have a third-party or a senior quality lead review the entire docket for completeness and internal consistency.
By treating the weld docket as a critical component of the engineering design rather than a secondary administrative task, you ensure safety, regulatory compliance, and project longevity.