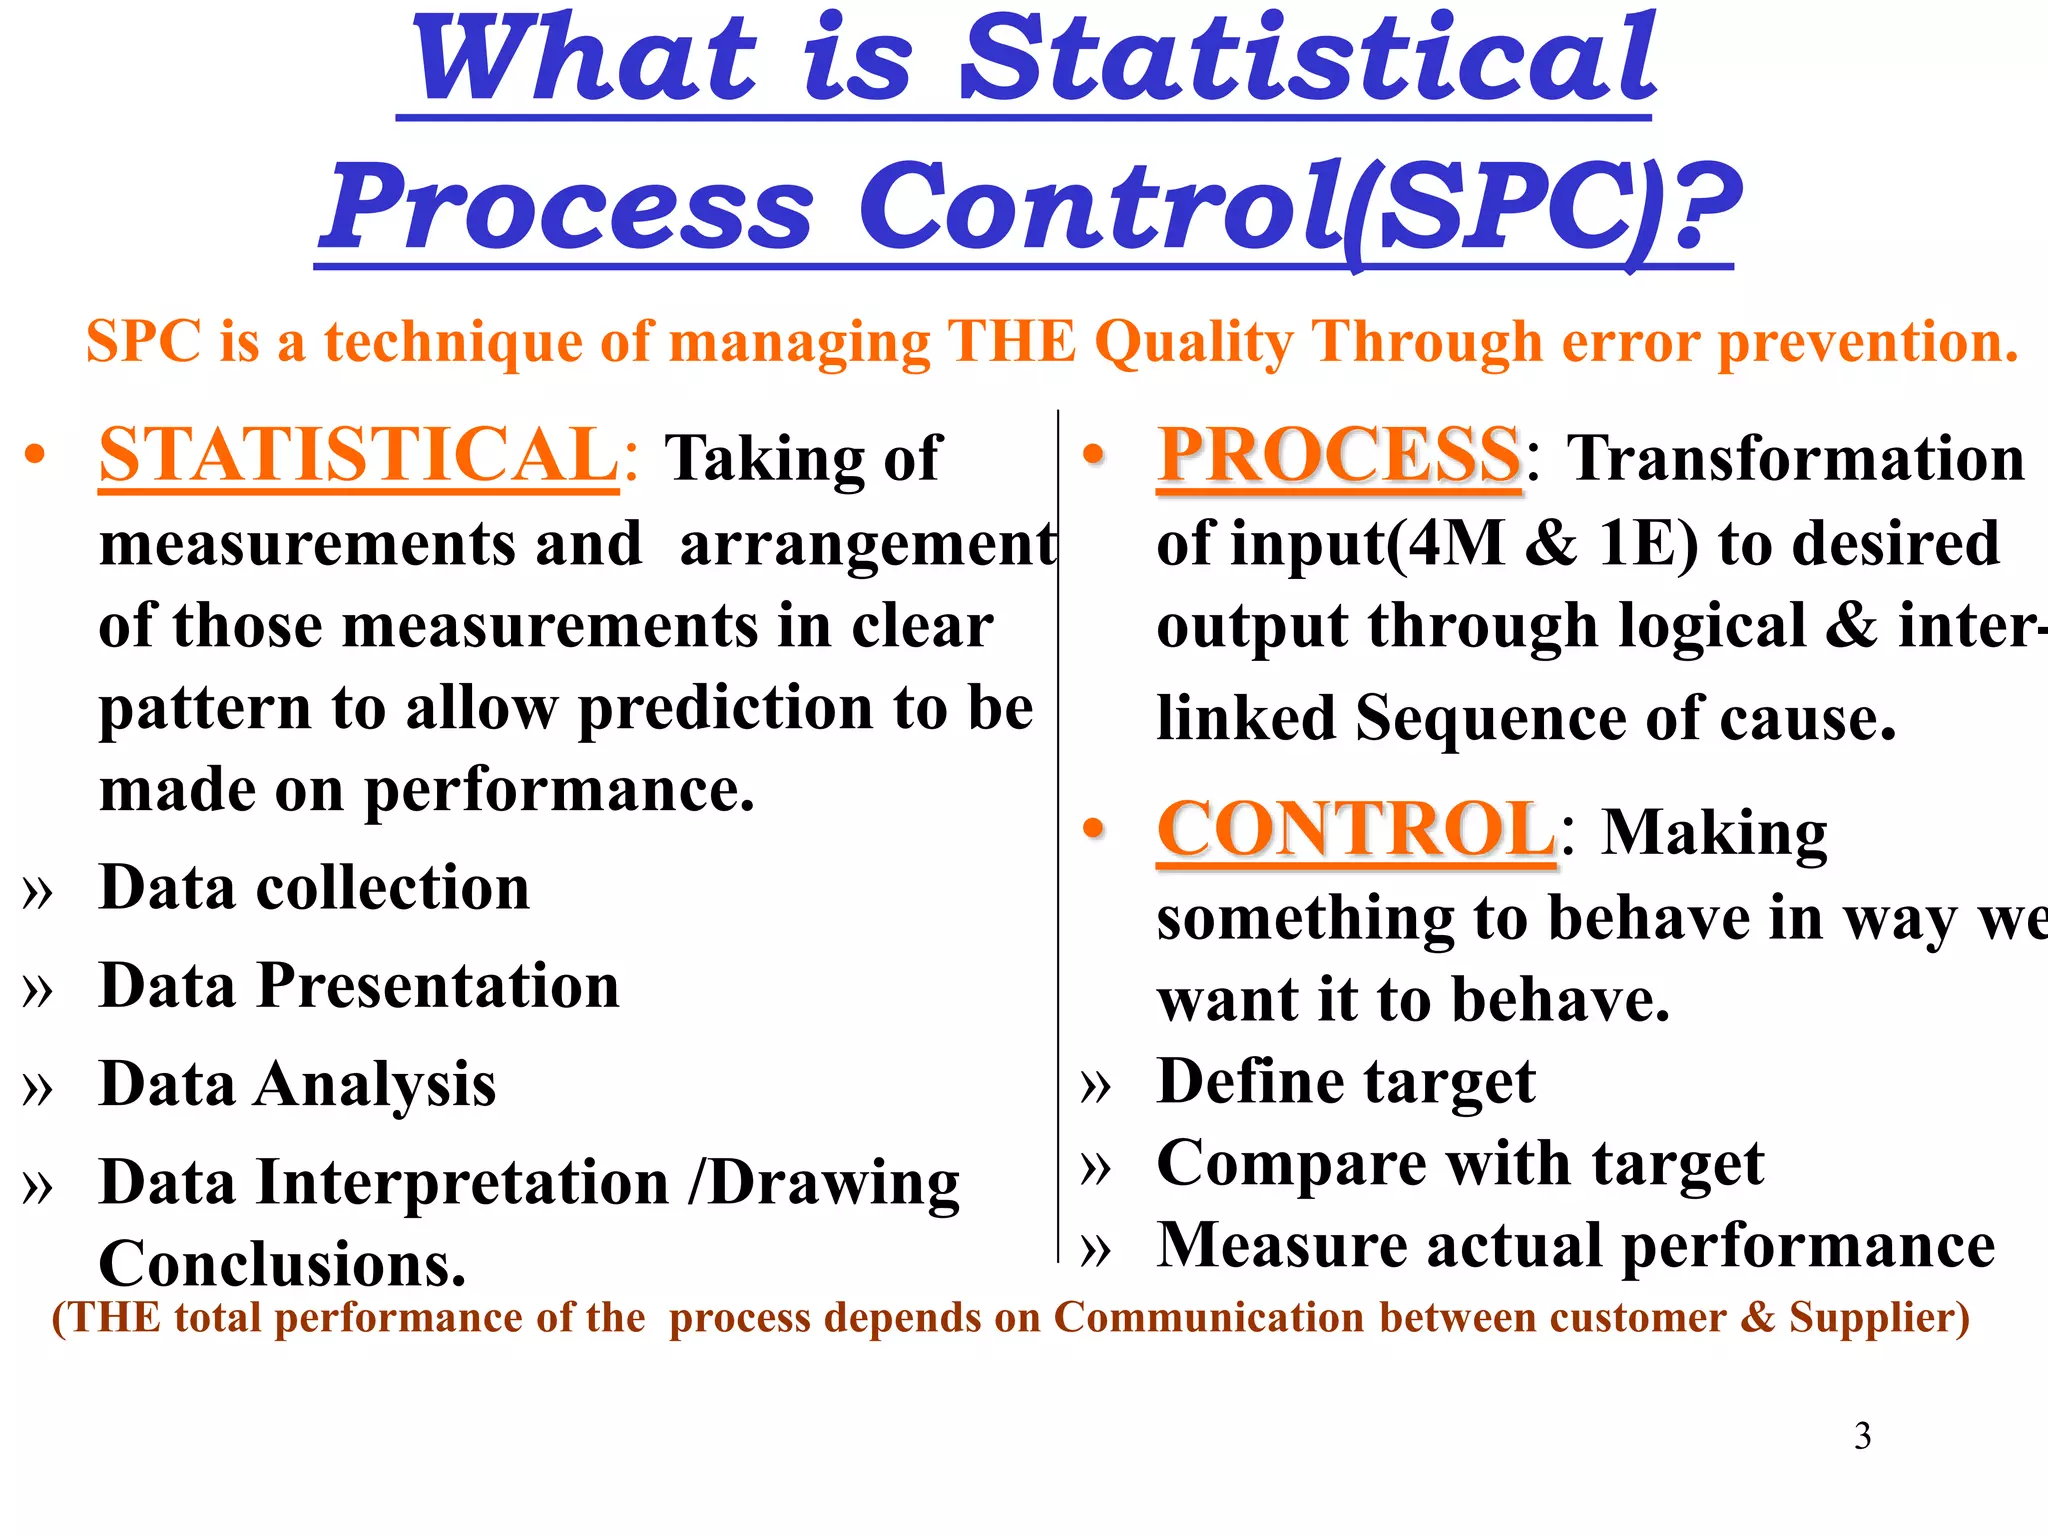
Statistical Process Control (SPC) is a data-driven methodology used to monitor, control, and improve manufacturing and business processes by identifying and reducing variation. By employing statistical analysis, practitioners distinguish between common-cause variation and special-cause variation, allowing them to make informed decisions that ensure output remains consistent with specifications and customer requirements.
The Fundamental Purpose of SPC
At its core, SPC is about stability. Every process—whether it is the thickness of a steel plate, the timing of a server response, or the fill level of a pharmaceutical bottle—exhibits variation. Without control, this variation can lead to defects, waste, and unpredictable quality. SPC provides the visual and mathematical tools to "listen" to the process.
When a process is operating under the influence of only "common causes"—the natural, inherent variation of a system—it is considered to be in a state of statistical control. However, when "special causes" (assignable, non-random events like a broken tool, a power surge, or a new employee error) intervene, the process becomes unpredictable. SPC tools alert operators to these special causes so they can intervene, restore stability, and prevent defective output before it reaches the customer.
Historical Context and Evolution
The origins of SPC date back to the 1920s at Bell Telephone Laboratories, where Dr. Walter A. Shewhart developed the concept of the control chart. Shewhart recognized that while variation is inevitable in any manufacturing process, it could be managed through probability theory. His work later became the foundation for quality control practices worldwide, championed by experts such as W. Edwards Deming.
While originally conceived for the factory floor, the application of SPC has expanded significantly by 2026. Today, the methodology is applied in service industries, healthcare quality assurance, and high-frequency data streaming. Despite these modern applications, the fundamental requirement remains the same: high-quality, time-sequenced data and a commitment to continuous process improvement.
Key Components of SPC Methodology
To implement SPC effectively, organizations rely on a specific set of tools and metrics. The methodology is not merely about tracking data but about interpreting that data against statistical limits.
1. The Control Chart
The control chart is the primary instrument of SPC. It plots process data points over time, typically showing a central line (the process average) and two horizontal boundaries known as the Upper Control Limit (UCL) and the Lower Control Limit (LCL).
- Center Line: Represents the mean or median of the process performance.
- Control Limits: These are calculated based on the standard deviation of the process data. They represent the boundaries of expected natural variation. If a data point falls outside these limits, the process is statistically "out of control."
2. Types of Variation
Understanding the two types of variation is critical to the SPC workflow:
- Common-Cause Variation (Systemic): Inherent to the process design. To reduce this, one must change the system, equipment, or materials.
- Special-Cause Variation (Assignable): External to the process. Examples include machine wear, operator fatigue, or raw material batch issues. This requires immediate investigation and corrective action.
3. Capability Analysis
While control charts determine if a process is stable, capability analysis determines if the process is capable of meeting customer specifications. A process can be in statistical control but still fail to meet product requirements if the process spread (the natural variation) is wider than the tolerance limits set by the engineer or the client.
Comparison of SPC Approaches
The choice of control chart depends largely on the type of data being collected and the nature of the process.
| Chart Type | Data Classification | Use Case |
|---|---|---|
| X-bar and R Chart | Variables (Continuous) | Monitoring the average and range of subgroup measurements. |
| I-MR Chart | Variables (Individual) | When subgrouping is impossible or cost-prohibitive. |
| p-Chart | Attributes (Pass/Fail) | Monitoring the fraction of nonconforming items in a sample. |
| c-Chart | Attributes (Count) | Counting the number of defects in a constant area of opportunity. |
Prerequisites for Successful Implementation
Implementing SPC is not a "plug-and-play" software solution; it requires a cultural shift and specific technical prerequisites. Organizations looking to adopt SPC in 2026 must ensure the following:
- Measurement System Analysis (MSA): Before analyzing data, one must verify the data itself. Through Gauge R&R (Repeatability and Reproducibility) studies, companies ensure their measurement tools are accurate and precise. If the gauge cannot measure the variation correctly, the resulting SPC charts will be misleading.
- Sampling Strategy: Practitioners must define how frequently data is collected. If samples are taken too far apart, special-cause variations might be missed. If they are taken too frequently, the cost of collection may exceed the value of the information.
- Employee Training: Operators must understand how to interpret control charts. They should know how to react to "out-of-control" signals and be empowered to stop a line when a process anomaly occurs.
Common Pitfalls and Troubleshooting
Even with robust systems, SPC programs often struggle due to human factors or misapplication. One common error is "tampering." This occurs when an operator adjusts a process based on every minor fluctuation, even when the data falls within control limits. This action actually increases the total variance of the process.
Another challenge is the "garbage in, garbage out" phenomenon. If the input data is missing timestamps, contains recording errors, or represents an unstable baseline, the control limits will be invalid. When troubleshooting an SPC implementation that seems to provide "false alarms," teams should:
- Re-verify the calibration of the measuring instruments.
- Review the stability of the input variables (e.g., raw material consistency).
- Ensure the subgrouping logic (how data is grouped for the charts) remains consistent with the physical process.
Operational Benefits and Limitations
The primary advantage of SPC is the move from "detection" to "prevention." In traditional quality control, a product is inspected at the end of the line, and defective units are scrapped. In an SPC-managed environment, the process is monitored in real-time. If a trend suggests that the process is drifting toward an out-of-tolerance condition, the operator can adjust the machine before a single defect is produced.
However, SPC has limitations. It does not replace the need for quality management systems or design excellence. If a product design is inherently flawed, SPC will merely monitor the production of a high volume of substandard parts with high consistency. Additionally, SPC requires a continuous commitment to data integrity, which can be resource-intensive for smaller enterprises or manual-heavy workflows.
Frequently Asked Questions
What is the difference between Control Limits and Specification Limits? Control limits are determined by the process itself—they represent how the process is actually performing. Specification limits are determined by the customer or design engineer—they represent what the product needs to be. A process can be in control and still produce parts outside of specification limits.
Can SPC be used in non-manufacturing settings? Yes. SPC is increasingly used in administrative processes and software development. For example, it can track the latency of API responses or the cycle time of help-desk tickets. If the average time deviates significantly, it signals a systemic issue in the process flow.
What is meant by an "out-of-control" process? An out-of-control process is one where the variation is no longer random. This is statistically signified by data points falling outside the control limits, or by patterns—such as a "run" of seven points in a row on one side of the center line—that suggest an assignable cause is influencing the outcome.
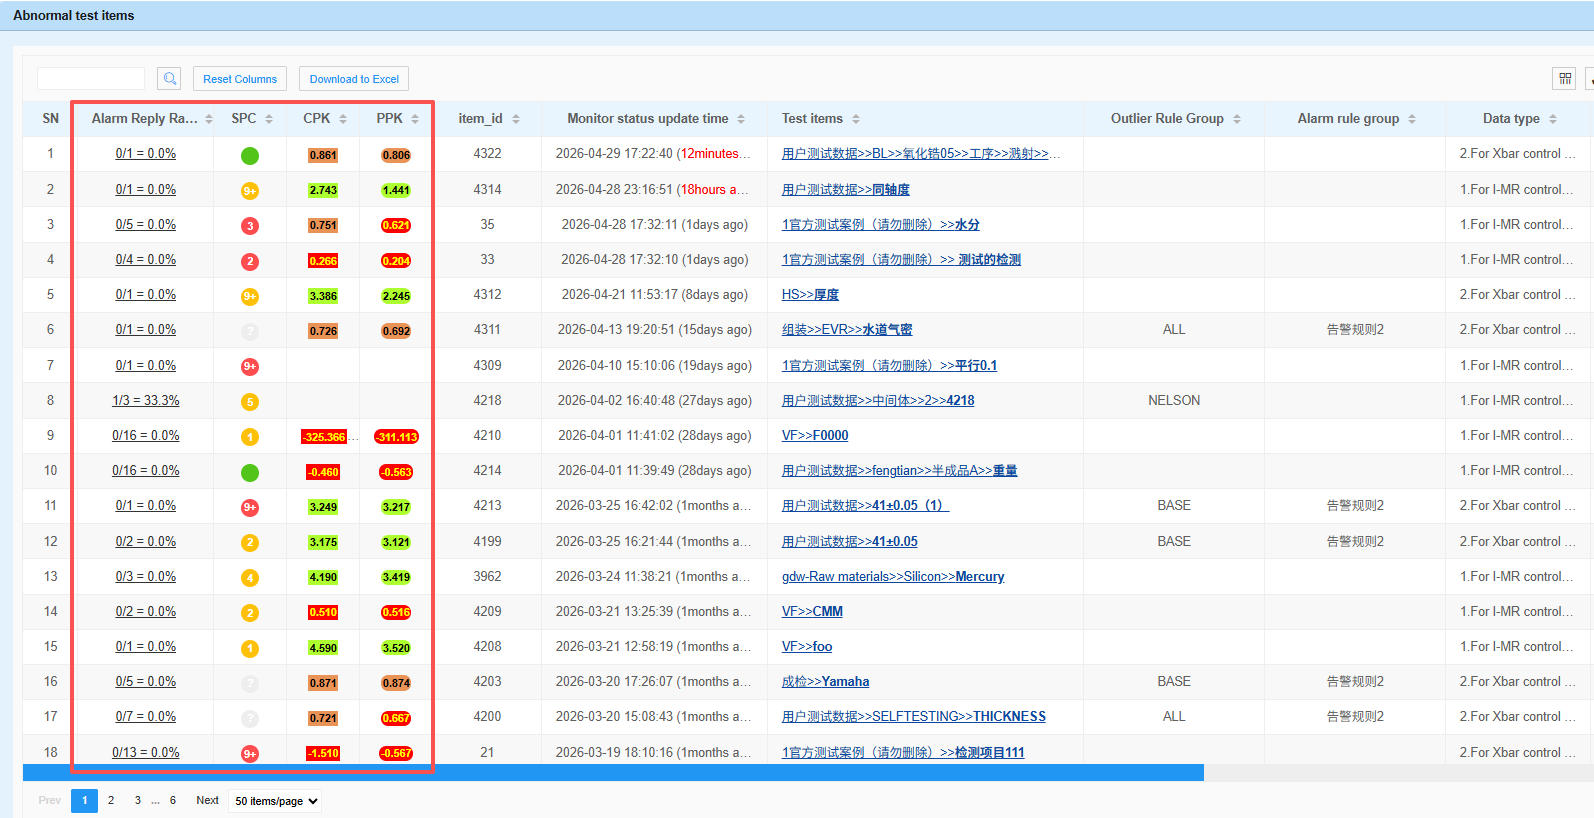
How does software change the implementation of SPC? Modern 2026-era SPC software automates the calculation of limits and triggers real-time alerts. This removes human error from the math side of SPC, allowing operators to focus on root cause analysis rather than manual data entry or graph plotting.
Is SPC mandatory for ISO certification? While ISO 9001:2015 does not strictly mandate the use of SPC, it requires organizations to monitor and measure processes to ensure they meet requirements. SPC is widely regarded as one of the most effective ways to satisfy these quality management requirements.
Next Steps for Implementation
To begin or improve your SPC journey, start by identifying a high-impact, high-variation process. Perform an MSA to confirm your measurement capability. Next, collect at least 20 to 25 data points to establish a baseline for your control charts. Once your charts are set up, focus on training your team to respond only to special-cause signals. By treating SPC as a strategy for continuous learning rather than just a compliance check, your organization can significantly reduce waste and improve long-term process capability.